ISO 9001
ISO 9001 Certified
Quality management system certified to international standards.
The standards, checks, and certifications behind every product across our brands.
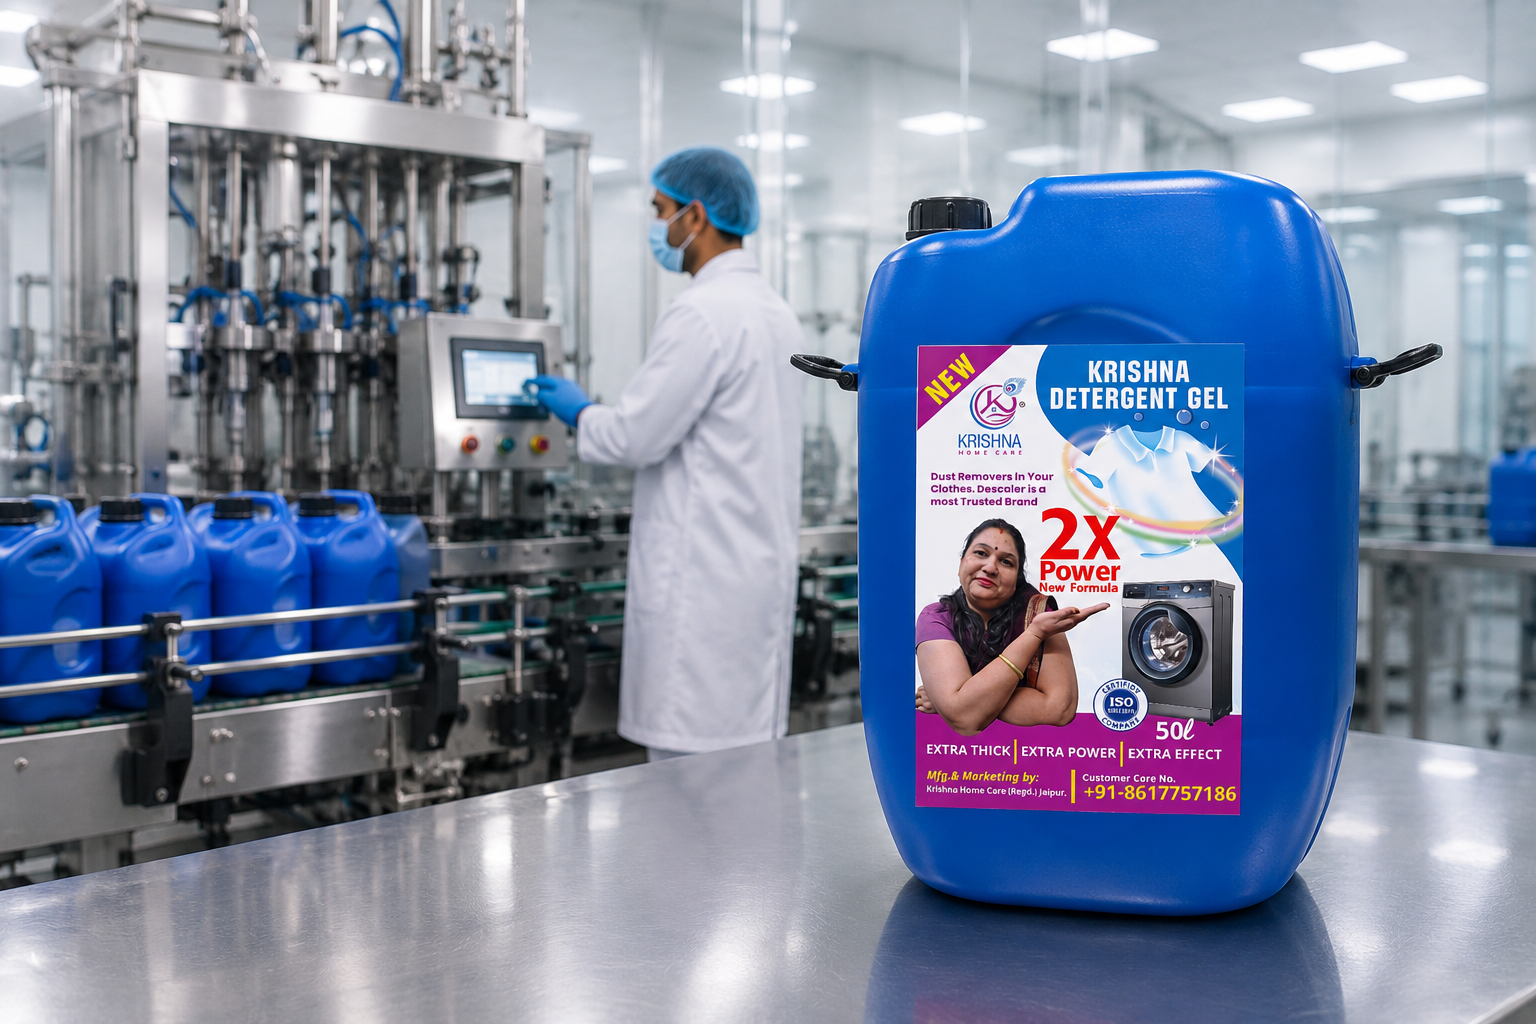
Every batch follows controlled, consistent production processes across facilities.
Dedicated testing at every stage, from raw material to finished product.
Manufacturing infrastructure built to support the group's growing brand portfolio.
Ingredients are sourced from trusted suppliers and checked before they enter production, so every batch starts from a consistent base.
Dedicated testing at every stage, from raw material to finished product.
Manufacturing facilities are maintained to strict hygiene and safety standards.
Standardised formulations mean the product you buy today performs the same as the one you bought last year.
Cans and bottles are sealed and checked to guard against leaks and tampering before they leave our facility.
Production is carried out under our ISO 9001 certified quality management system.
Quality management system certified to international standards.
Recognised for excellence in the home care products category.